Sizing tools
Electrode and amperage
Tell us the thickness and material and we'll tell you which electrode to use, at what amperage and on which machine.
Set the thickness and choose material and position.
Material
Welding position
Electrode
Ø 2.5mm
3/32"
Amperage
70-110A
Start at 90 A
Suggested type
E6013
E6013 / E6011
💡E6013 for general work and a clean bead; E6011 when the plate is rusty, painted or damp.
| Electrode | Inches | Amperage | Thickness |
|---|---|---|---|
| Ø 1.6 mm | 1/16" | 40-70 A | 0.8-2 mm |
| Ø 2 mm | 5/64" | 50-90 A | 1.5-3 mm |
| Ø 2.5 mm | 3/32" | 70-110 A | 2-5 mm |
| Ø 3.2 mm | 1/8" | 90-150 A | 3-8 mm |
| Ø 4 mm | 5/32" | 130-200 A | 6-14 mm |
| Ø 5 mm | 3/16" | 180-270 A | 10-25 mm |
Machines that deliver it
Best fit DIGIMIG 140MMA / FCAW / Lift TIG multi-process inverter welder140 A · 110/220 V · MMA / FCAW / TIG Lift Arc
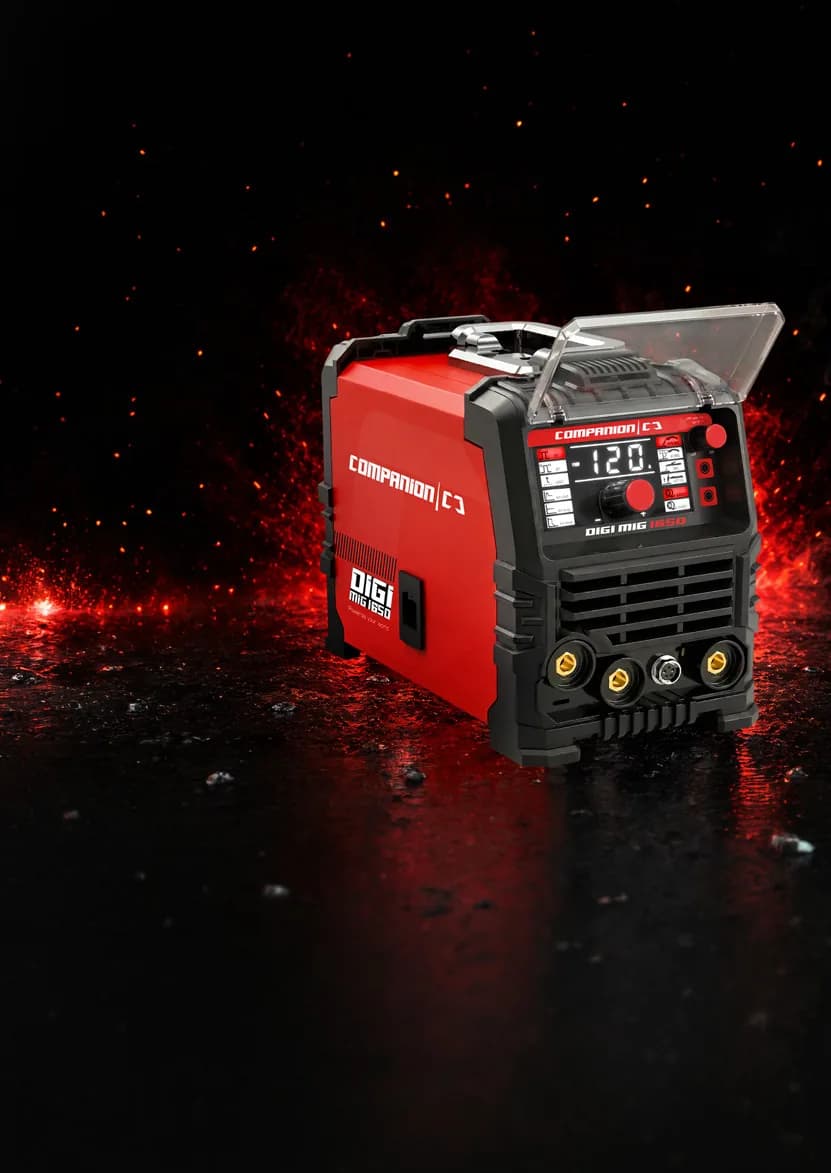 DIGIMIG 1650MMA / FCAW / Lift TIG multi-process inverter welder160 A · 110/220 V · MMA / FCAW / TIG Lift Arc
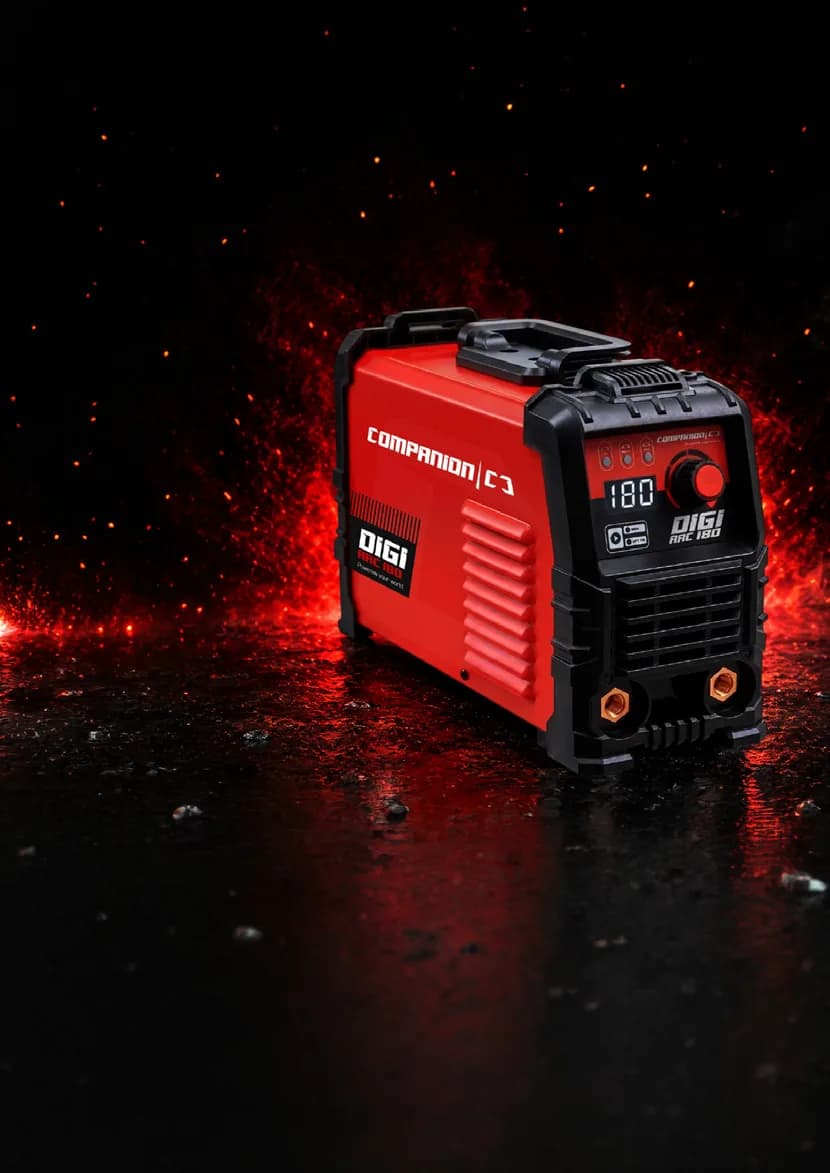 DIGIARC 180MMA / Lift TIG inverter welder180 A · 110/220 V · MMA / TIG (Lift Arc)
DIGIMIG 140MMA / FCAW / Lift TIG multi-process inverter welder140 A · 110/220 V · MMA / FCAW / TIG Lift ArcDIGIMIG 1650MMA / FCAW / Lift TIG multi-process inverter welder160 A · 110/220 V · MMA / FCAW / TIG Lift ArcDIGIARC 180MMA / Lift TIG inverter welder180 A · 110/220 V · MMA / TIG (Lift Arc)Complete the kit


Starting values: fine-tune by penetration, bead appearance and the electrode maker's recommendation. Vertical and overhead call for lower amperage and narrower beads.